Prodrive Technologies, while a comparatively new name in machine vision, has been around for more than 30 years, beginning life as a production and research partner for high-end electronics in the semiconductor industry. It has its headquarters in the Netherlands, with regional hubs in the USA, Japan, Malaysia and China.
The entire business now serves embedded computing systems, power conversion and manufacturing services, with its advanced cameras sitting in its precision solutions division.
Prodrive’s machine vision expertise grew from experience in this sector and, with multiple manufacturing sites, was able to build its own products from the ground up, ensuring its own high standards have always been met with this part of the business.
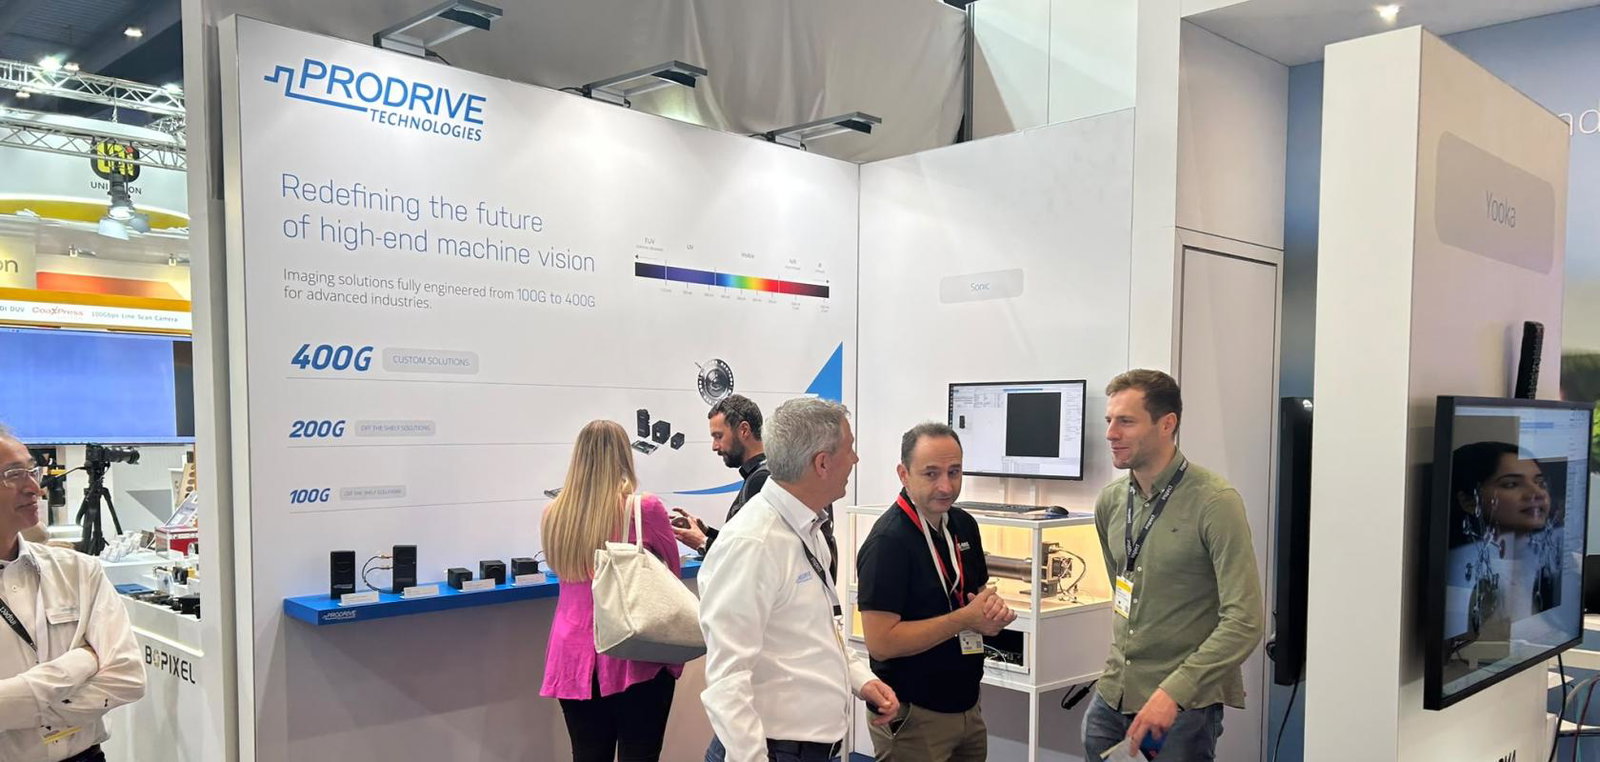
Prodrive’s tagline for its camera activities is ‘Stay Ahead of the Field’, supported by the VISION 2026 theme ‘Redefining the Future of High-End Machine Vision’. Marco van Hout, Global Sales Manager for advanced cameras, says: “The booth at this year’s show reflects our commitment to pushing the boundaries of machine vision technology. Visitors have experienced the full breadth of our imaging solutions portfolio, ranging from 100 Gbit/s to 400 Gbit/s, showcasing how our technologies scale from high-speed imaging products to highly customised solutions that support our customers to stay ahead of the field in their market.”
Its wider experience in the electronics industry means Prodrive can genuinely position itself as a long-term technology partner. “The performance and flexibility of our solutions helps customers stay ahead in an increasingly competitive and data-driven market,” adds van Hout.
From a product perspective, Prodrive focused on two key solutions. “‘First, we introduced the Runix MX, our latest high-resolution camera platform featuring 105 megapixels,” says van Hout. “It is the first member of a new product line designed for applications that require exceptional image quality and performance. In addition, we showcased a live demonstration of our Yooka platform in a 200G application, demonstrating how high-speed imaging can be used in demanding industrial machine vision environments.”
The Yooka platform offers up to 2,000fps in full resolution using the GSprint sensor and boasts capture rates of 30,000fps at resolutions up to 21MP. Runix, with resolutions up to 105MP, focuses on large area scan combined with high pixel rates for metrology solutions in semiconductor and flat panel display processing, as well as scientific imaging. “Together, these demonstrations showcased our ability to deliver high-performance imaging solutions that help customers tackle increasingly complex inspection and automation challenges,” concludes van Hout.
Beyond these, Prodrive can also provide fully customised solutions, including the integration of custom sensors, developed entirely by an in-house engineering team. Its primary applications are in the semiconductor and life science industries and include cameras for E-beam, DUV, visible and IR imaging.
Prodrive sets itself apart from its competitors in a number of ways, according to van Hout: “What differentiates us is our combination of deep imaging expertise, vertical integration, and system-level engineering capabilities. We go from components to systems by combining cameras, motion control, software, and custom engineering into complete opto-mechatronic solutions.”